Sheet metal solutions
Flexible sheet-metal fabrication
Balance cutting and bending with programming, tool changes and sorting. Choose equipment around your mix of short runs, repeat orders and changing drawings.
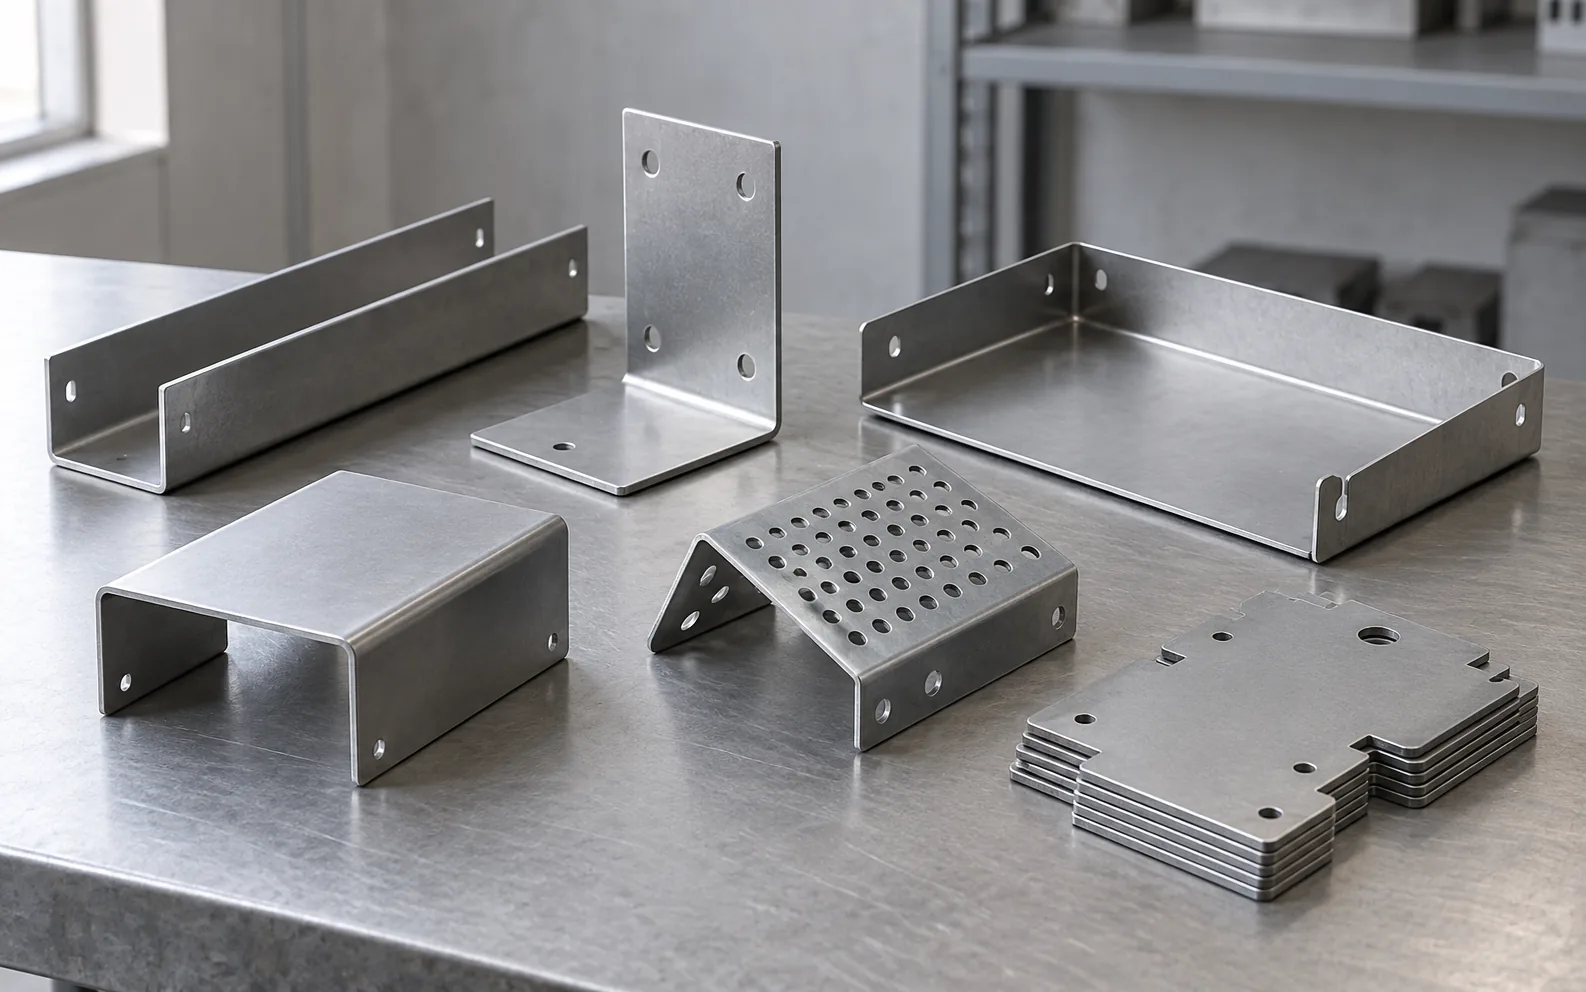
Start with the parts you make
A useful job-shop brief includes both the repeat work and the awkward one-off parts that consume setup time.
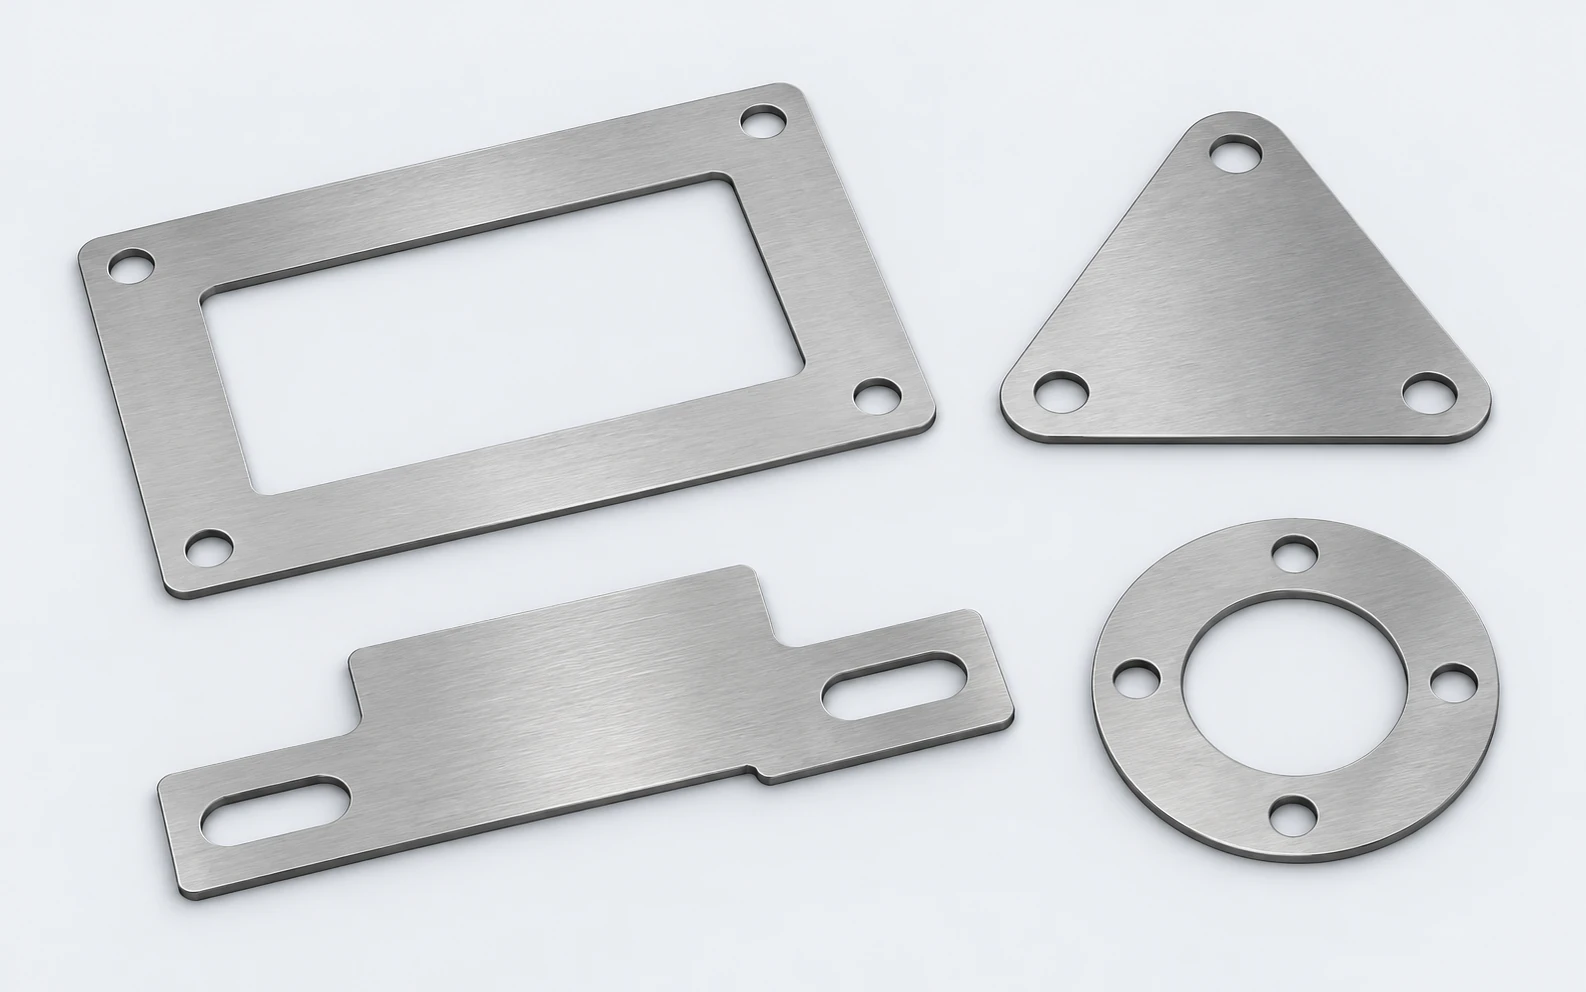
Profiled sheet parts
Group common material grades and thicknesses, then identify small features and surface requirements that need a different setup.
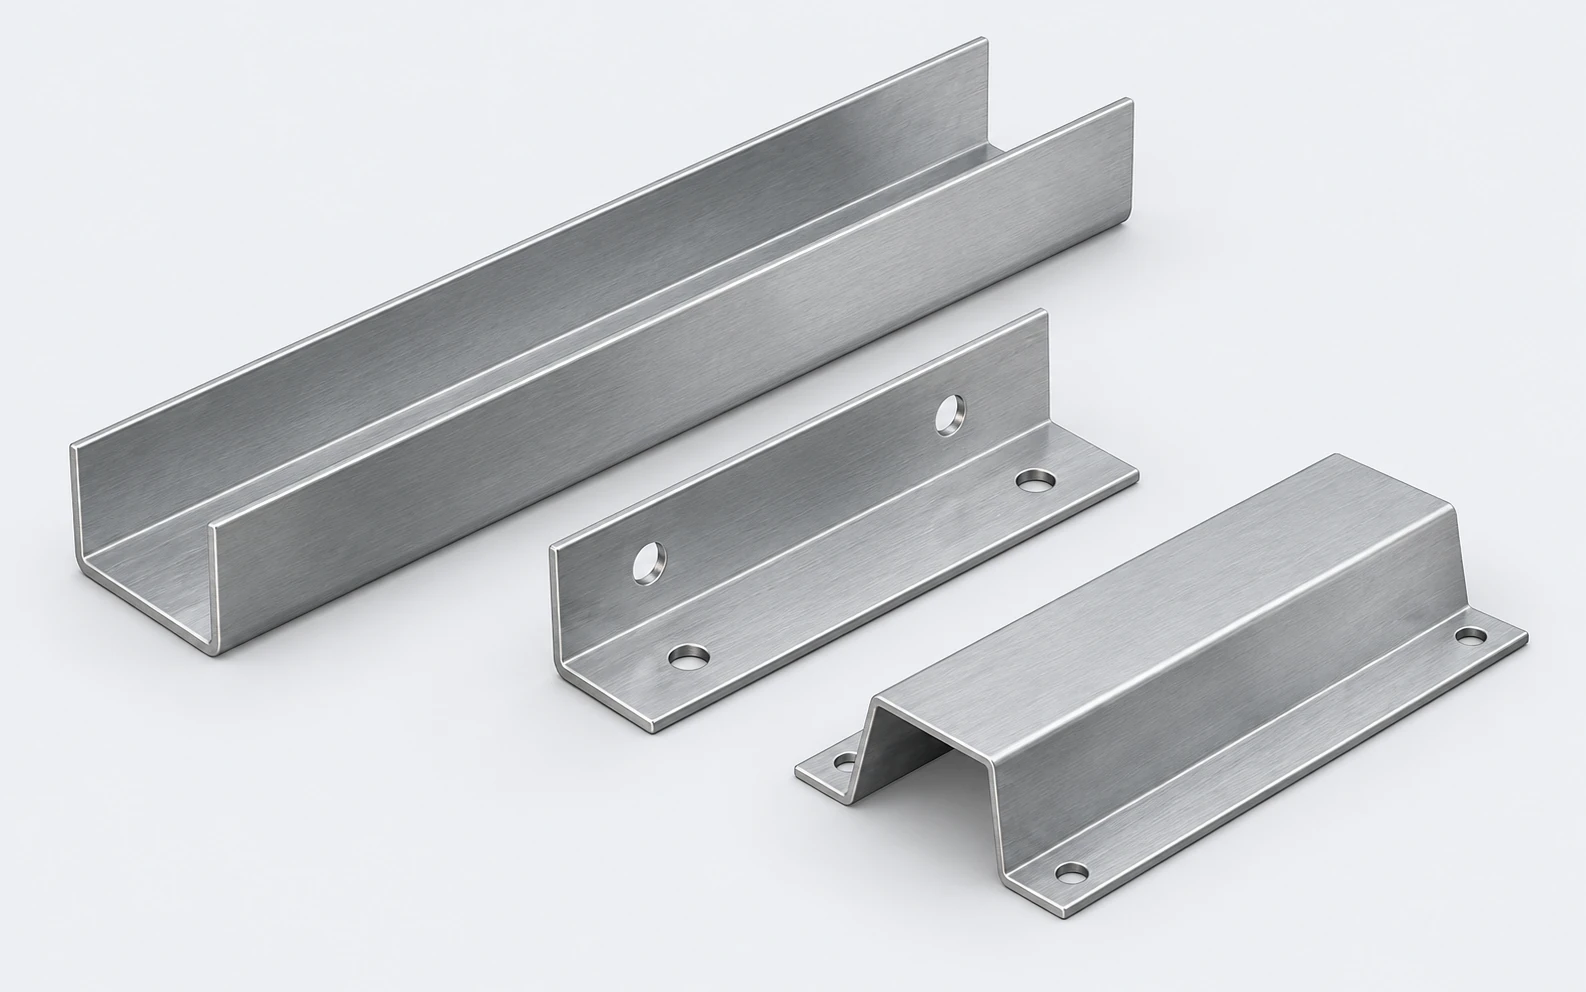
Folded brackets and channels
Compare bend sequences and tool access across small parts, long folds and the shapes that change most often.
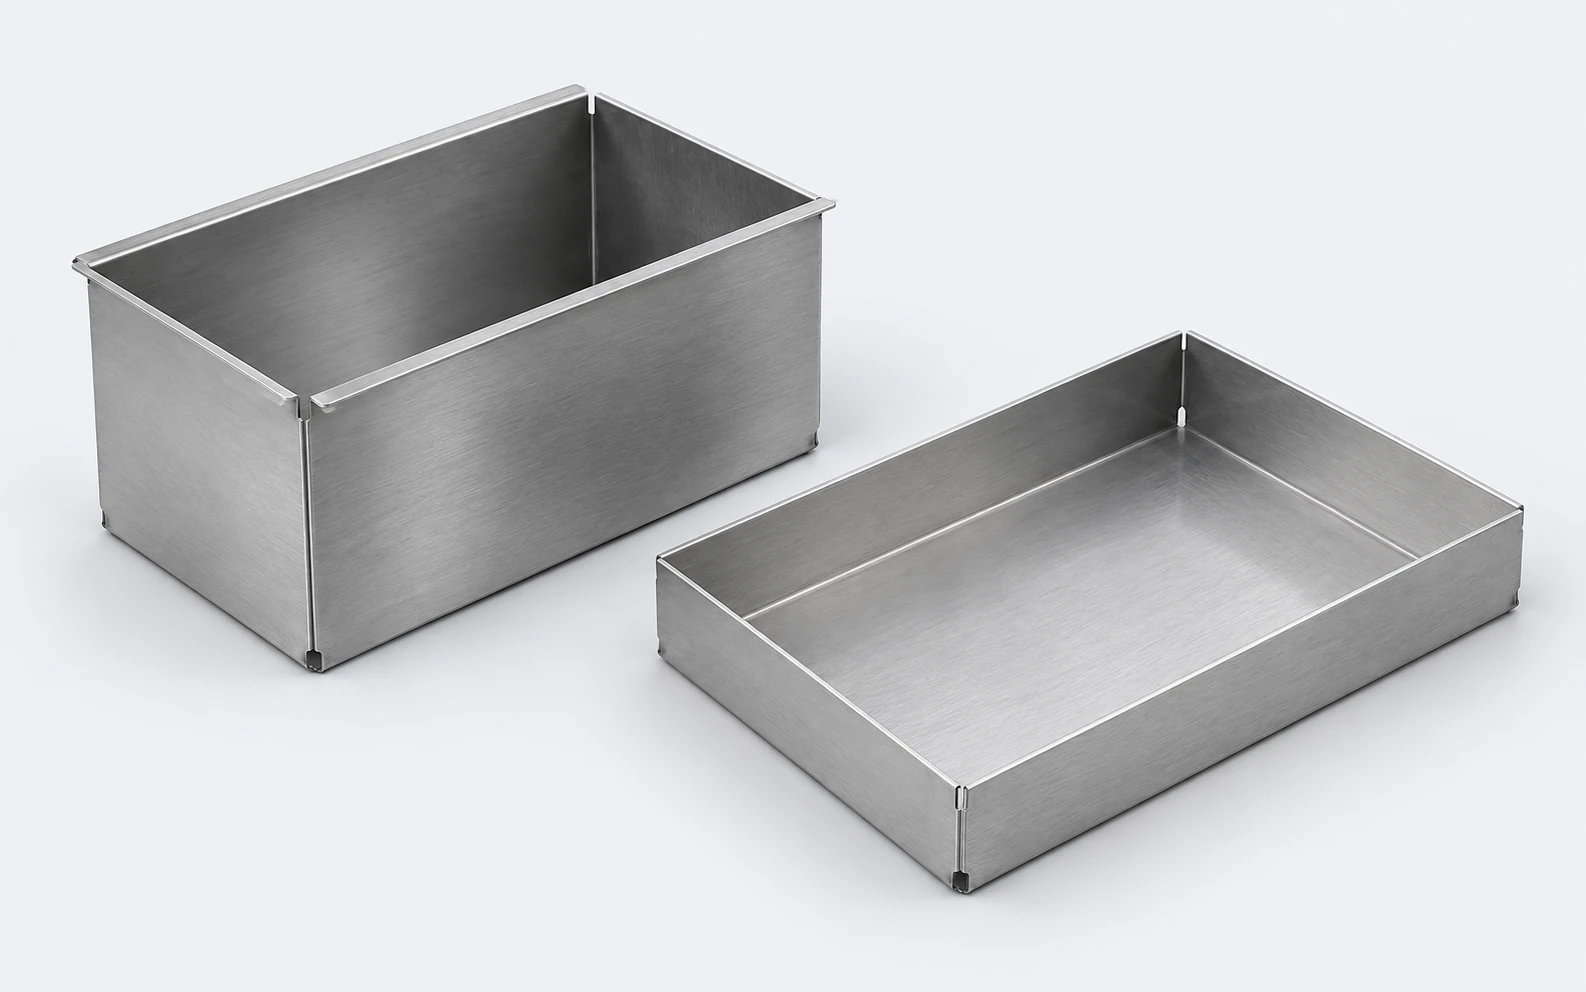
Boxes and trays
Review return flanges, part handling and whether suitable panel families justify a separate forming method.
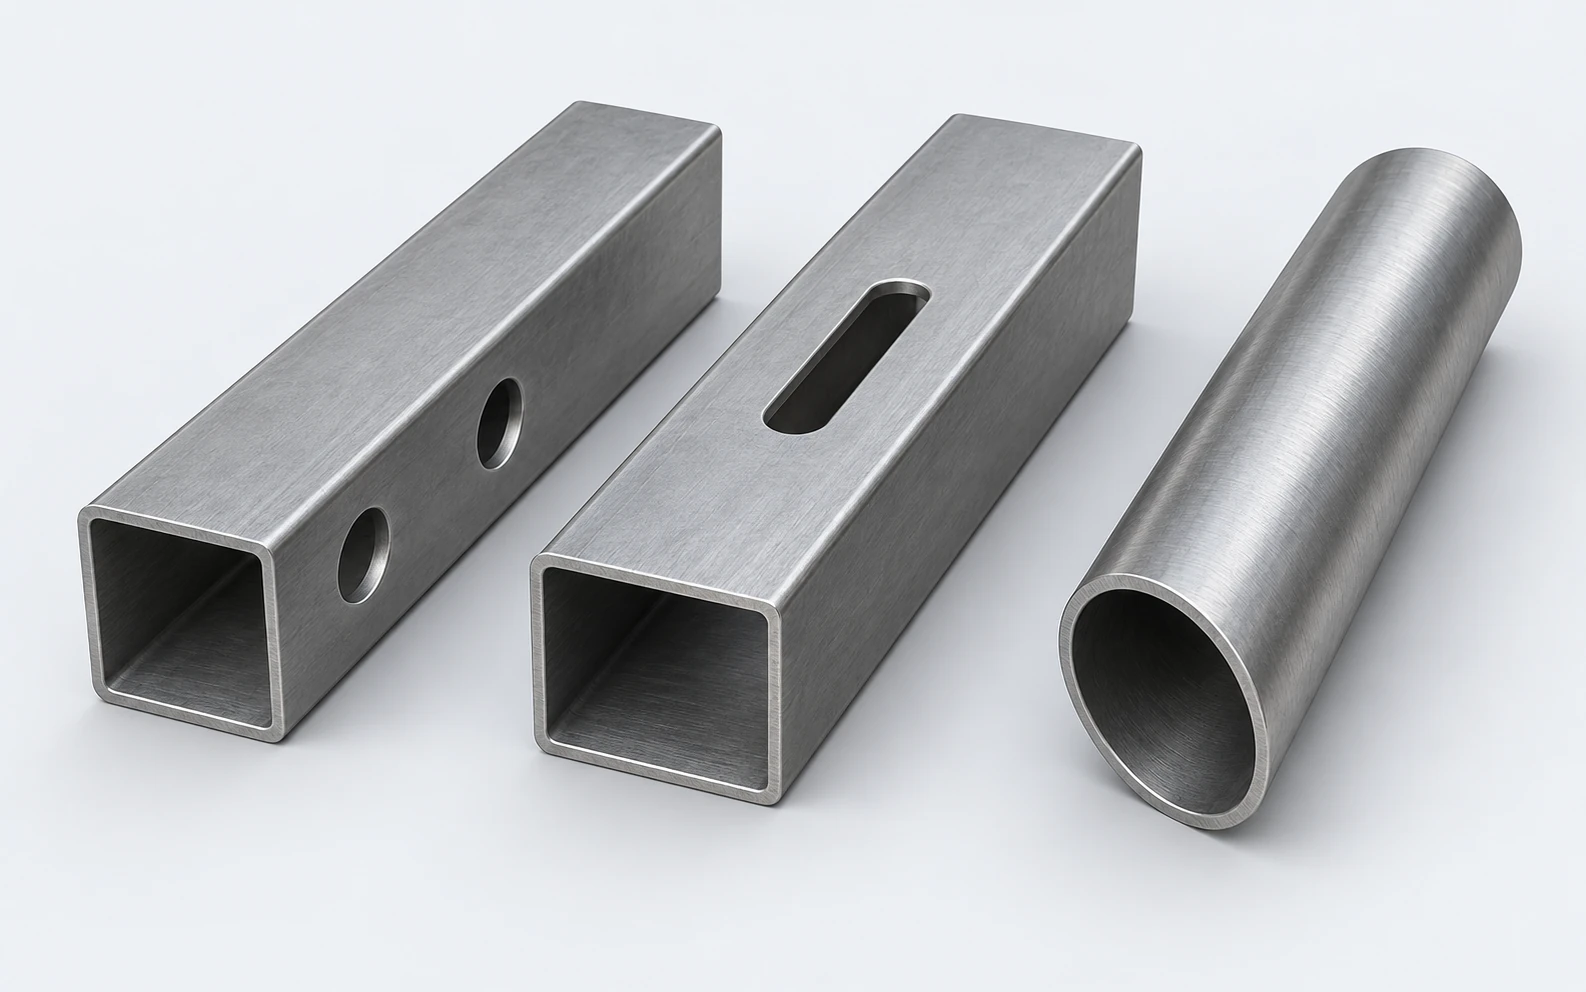
Tube components
Keep tube sizes, lengths and profiles distinct from sheet work; include the required end cuts and mounting features.
Connect the part to the process
Frequent changeovers
Record programming, material loading, tool changes and first-part checks separately. The machine cycle is only one part of completing a short order.
Uneven workloads
Look at queues between cutting, sorting and bending. Adding speed at one station may leave the actual bottleneck untouched.
A wide part envelope
Use the normal workload and the limiting parts together. A machine selected only for an unusual job can be a poor fit for daily production.
Choose the equipment for each task
Group jobs by material and setup, choose the cutting and bending route for each part family, and plan sorting so the next operation receives identifiable parts.
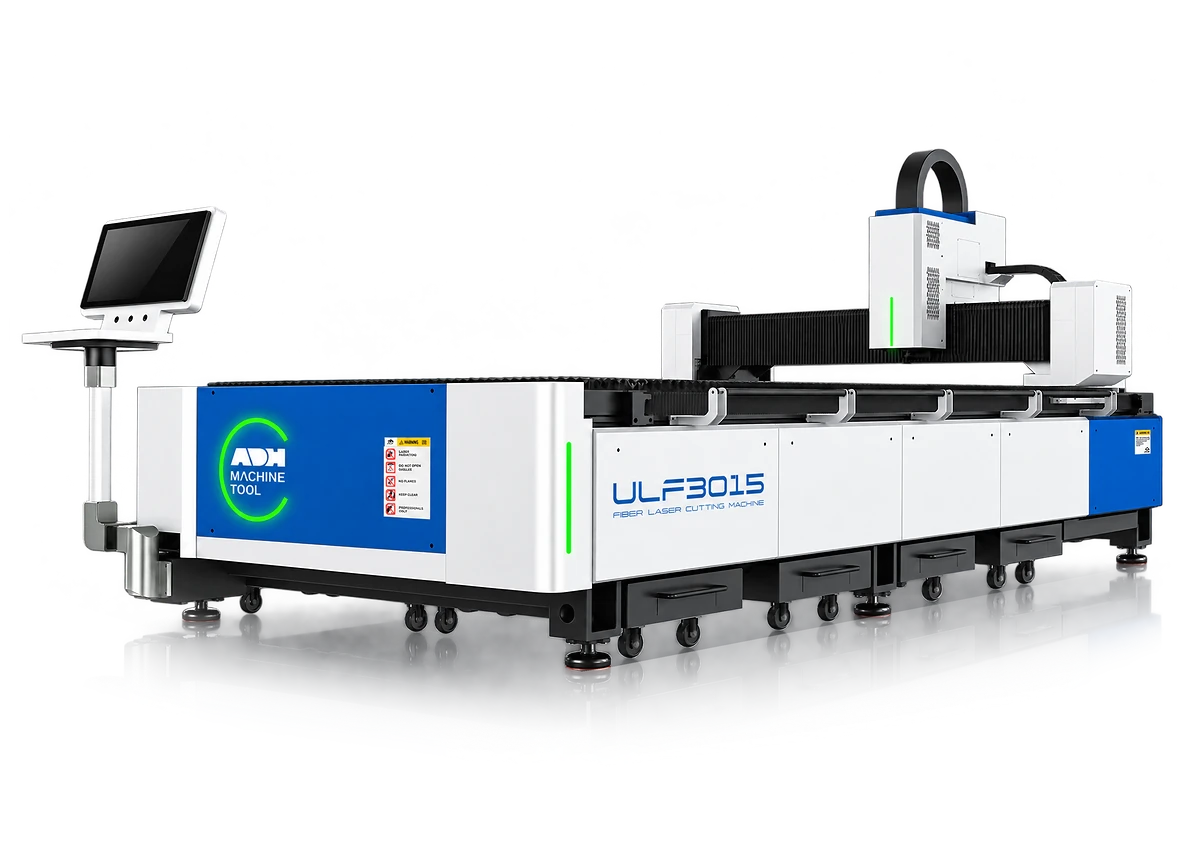
Cut a varied sheet workload
Compare laser systems by material range, working format and loading method. Include programming and the effort to separate finished parts from the sheet.
Compare laser cutting systems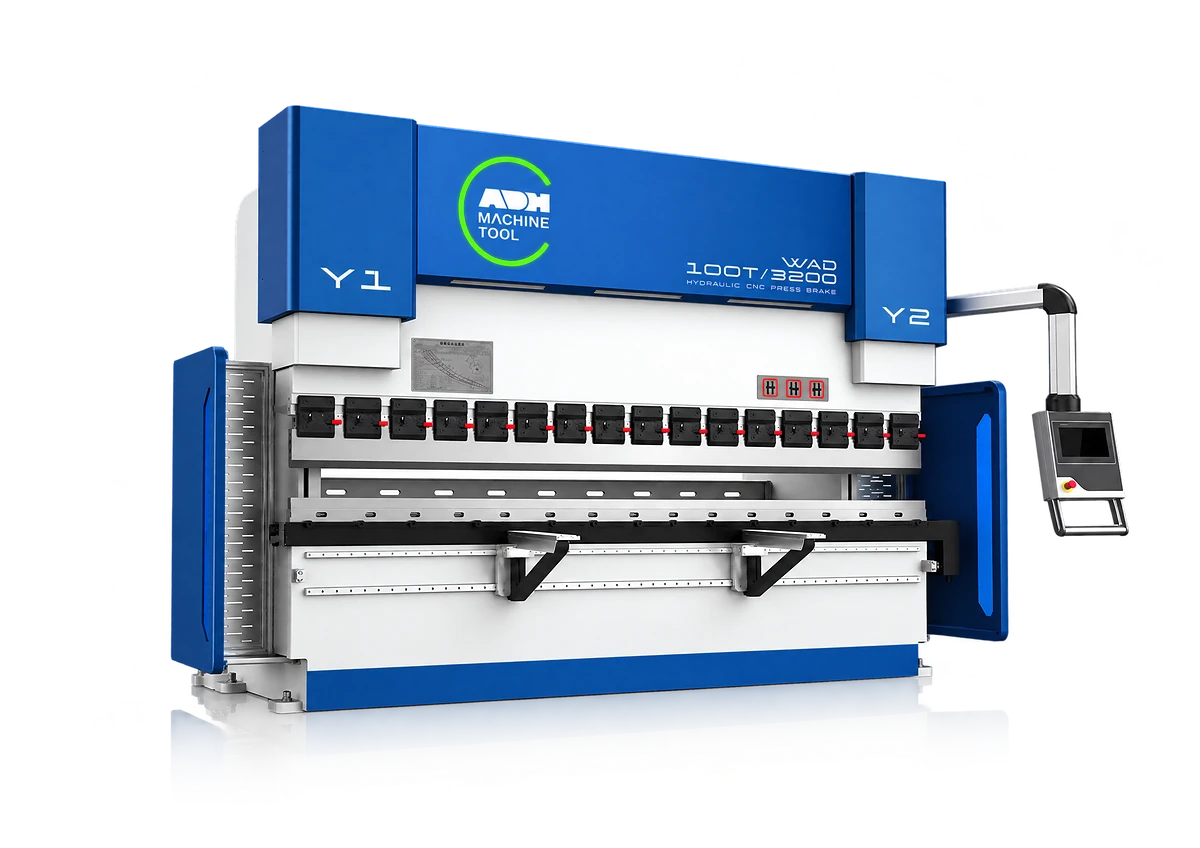
Bend changing part shapes
A CNC press-brake comparison should include tooling, program preparation, backgauge access and first-part inspection across the actual mix.
Compare CNC press brakes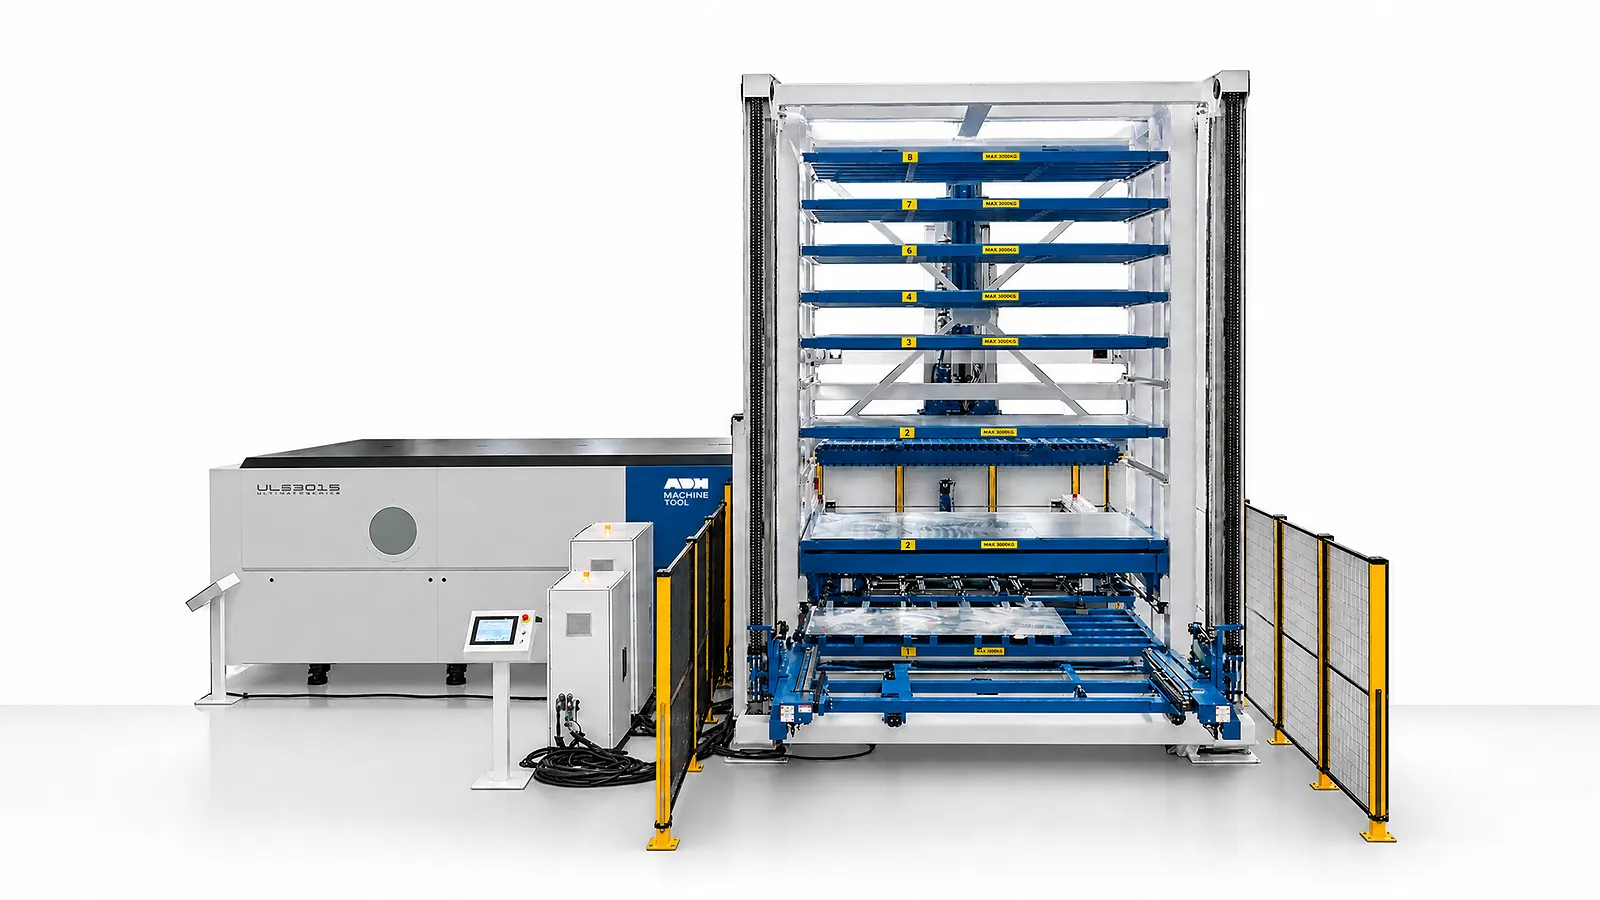
Automate a defined handling task
Consider laser FMS only after identifying the storage, loading and unloading work to be automated. Include remnants, sorting and recovery from exceptions.
Explore laser FMSA shop can improve one station before connecting a cell. Keep sheet and tube demand separate when comparing a combined machine with dedicated equipment.
A customer’s plate and tube workflow
Suzhou Guantuo’s project in China describes separate plate and tube laser equipment, staffing and reported production measures. It offers a concrete comparison for shops planning both types of work.